Groupleefkimyadisticaret.com: Your Trusted Mining Chemical Company for Superior Solutions and Industry Leadership
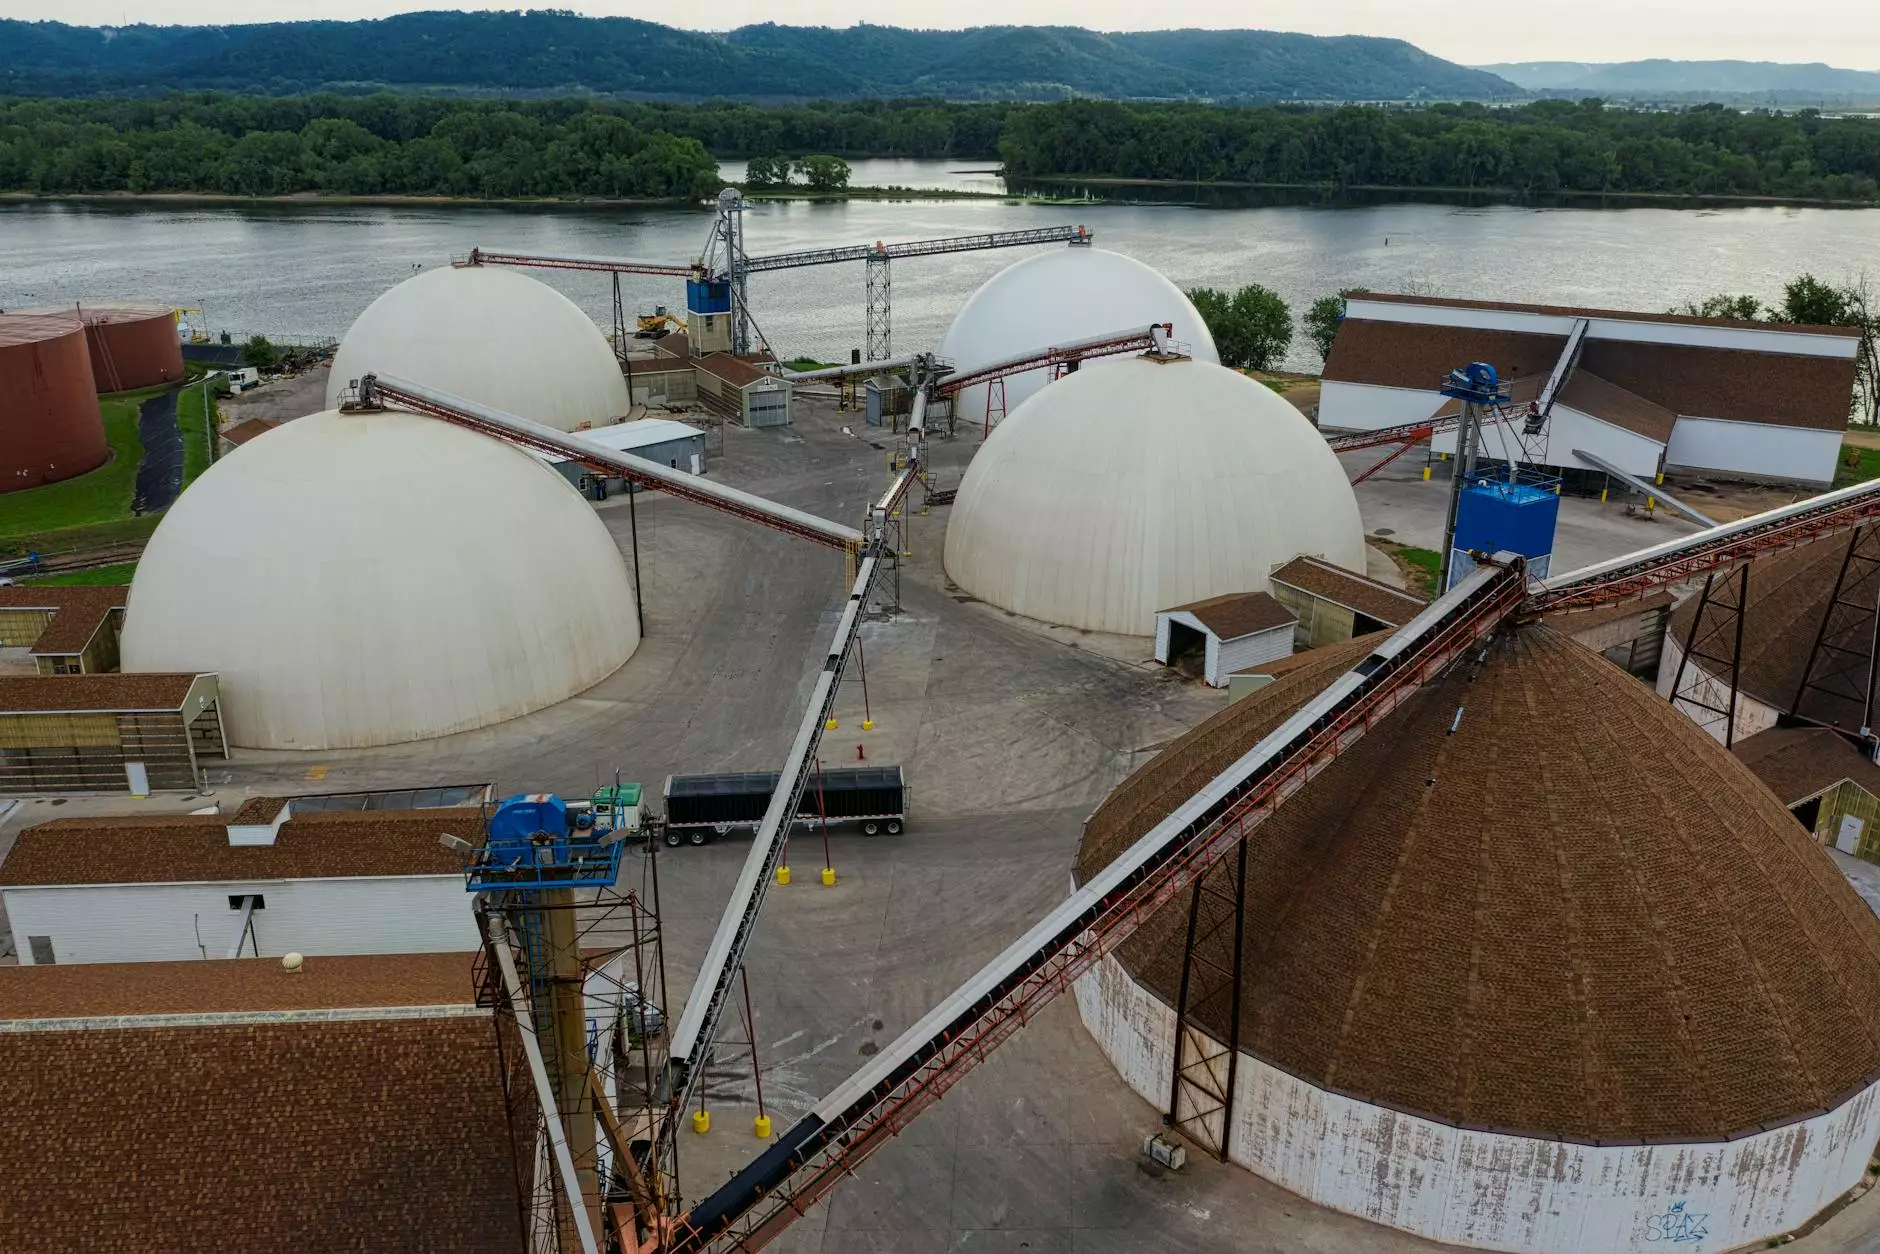
In the modern mining industry, the demand for high-quality, reliable chemical solutions is more critical than ever. Mining operations worldwide require a range of specialized chemicals to enhance efficiency, ensure safety, and maximize environmental compliance. Groupleefkimyadisticaret.com stands out as a leading mining chemical company dedicated to providing innovative, sustainable, and high-performance chemical products tailored specifically for the mining sector.
Why Choose Groupleefkimyadisticaret.com as Your Mining Chemical Company
Being a chemicals expert in the mining industry, our company understands the unique challenges faced by mining companies. Our commitment to excellence, safety, and environmental responsibility sets us apart. Here’s why customers trust us:
- Extensive Expertise: Over two decades of specialized experience in manufacturing and distributing mining chemicals.
- Innovative Product Development: Continuous research and development to provide cutting-edge chemical solutions that meet evolving industry needs.
- Quality Assurance: Robust quality control systems ensuring compliance with international standards such as ISO 9001, ISO 14001, and industry-specific certifications.
- Environmental Responsibility: Commitment to eco-friendly chemicals that reduce environmental impact during mining operations.
- Global Supply Network: Efficient logistics and global distribution channels for timely and cost-effective delivery worldwide.
Comprehensive Range of Mining Chemicals Offered by Groupleefkimyadisticaret.com
At Groupleefkimyadisticaret.com, we manufacture a broad portfolio of chemicals designed explicitly for the mining industry. Our products empower mining companies to optimize their processes, enhance safety, and promote environmental sustainability.
Key Categories of Mining Chemicals
- Flotation Reagents: Essential for mineral separation, our flotation chemicals improve the recovery rate of valuable minerals. Types include collectors, frothers, modifiers, and depressants.
- Leaching Agents: Oxidizers and acids designed for efficient ore leaching processes, increasing metal yields while maintaining safety standards.
- Mining Process Additives: Including grinding aids, scale inhibitors, and corrosion inhibitors that optimize operational efficiency and equipment lifespan.
- Water Treatment Chemicals: Coagulants, flocculants, and pH adjusters that ensure water used in mining is treated effectively, reducing pollutant levels and minimizing environmental impact.
- Explosives and Detonators Chemicals: Specialized chemicals used in controlled blasting, maximized for safety and precision.
Advanced Technologies in Mining Chemicals
Our R&D team at Groupleefkimyadisticaret.com relentlessly pursues innovation to develop products that meet and exceed industry standards. Our advanced chemical formulations ensure better mineral recovery, lower reagent consumption, and reduced environmental footprint.
Sustainable and Eco-Friendly Chemical Solutions
Environmental sustainability is at the core of our operations. We focus on producing eco-friendly chemicals that maintain high performance while minimizing ecological impact. Our bio-based flotation reagents, biodegradable water treatment chemicals, and reducing agents exemplify our commitment to sustainable practices.
Application of Our Chemicals Across Different Mining Types
Our chemicals cater to various mining environments, including:
- Metallurgical Mines: Copper, gold, iron, zinc, and other metal ore processing.
- Coal Mining: Flotation agents, dust suppressants, and water treatment chemicals tailored for coal extraction.
- Rare Earth Elements: Specialized reagents for extracting and processing these critical minerals efficiently.
- Industrial Minerals: Chemicals designed for processing talc, limestone, phosphates, and more.
The Benefits of Partnering with Groupleefkimyadisticaret.com
Choosing the right mining chemical company can significantly influence your operational success. Our partnership offers numerous advantages:
- Custom Solutions: We customize chemical formulations to fit your specific mining needs and ore characteristics.
- Expert Technical Support: Our team of chemists and industry specialists provides ongoing technical assistance and optimization strategies.
- Cost Efficiency: Our innovative formulations reduce reagent consumption and operational costs.
- Compliance and Safety: All products adhere strictly to safety and environmental regulations, ensuring safe handling and disposal.
- Reliable Supply Chain: We guarantee timely delivery regardless of project scale or location.
Industry Leadership and Commitment to Quality
As a frontrunner in the chemicals sector for mining, Groupleefkimyadisticaret.com continually invests in technology, sustainability, and workforce training to maintain our leadership position. Our dedication to quality is evident through rigorous testing, quality control measures, and adherence to international standards.
Future Trends in Mining Chemicals and Our Role
The future of the mining industry is geared towards sustainable development, automation, and digitalization. Groupleefkimyadisticaret.com is proactively developing chemicals compatible with these trends, including smart reagents that adapt to various ore types and environmental conditions, and biodegradable products that align with global eco-friendly initiatives.
Conclusion: Why Groupleefkimyadisticaret.com Is Your Premier Mining Chemical Company
In summary, selecting the right mining chemical company is crucial for operational efficiency, safety, and sustainability. Groupleefkimyadisticaret.com combines expertise, innovation, quality, and environmental responsibility to deliver exceptional chemical solutions tailored to your mining projects. We are committed to supporting your success by providing products that meet the highest standards and adapt to future industry needs.
Partner with us today for reliable, efficient, and sustainable chemical solutions that propel your mining operations forward, ensuring they are profitable, safe, and environmentally conscious.


